Optimizing Shop Drawings with DFM (Design for Manufacturability) Guidelines to Reduce 90% of RFIs on the Shop Floor
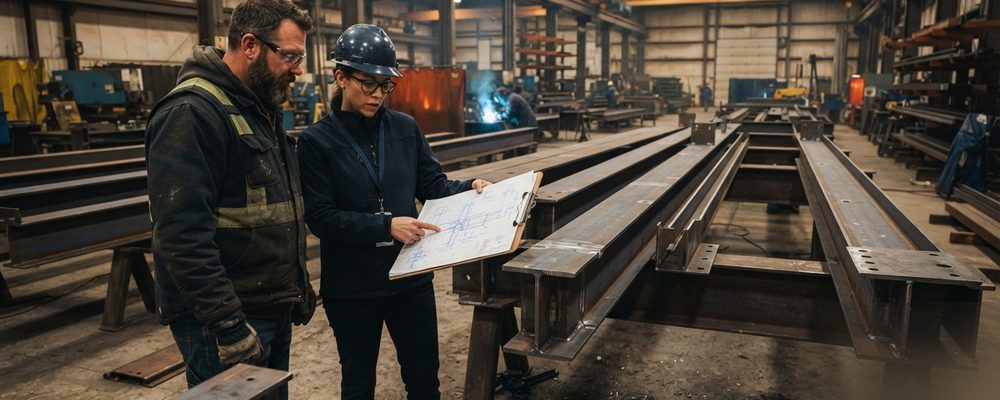
- DFM-optimized shop drawings spell out weld type, direction and stagger pitch so fabricators never have to guess or file an RFI.
- Bend specifications need K-factors and bend allowances worked out up front, with clear tolerances for critical bends.
- Drawings should be complete but not cluttered — excess non-fabrication detail slows machine operators down as much as missing detail does.
Design for Manufacturability (DFM) in steel fabrication bridges the gap between conceptual engineering and practical shop-floor execution. When CAD detailers incorporate DFM rules, shop drawings provide explicit instructions for cutting, drilling, punching, bending, and welding without requiring constant clarification.
Welding & Joining Instructions
Shop drawings must clearly define weld types—such as groove, fillet, spot, seam, slot, or plug welds—and specify weld directions and filler electrode requirements. For intermittent welding, detailers must specify the exact length and pitch of staggered welds to prevent thermal material distortion.
Bending Specifications & Tolerances
Accurate bend calculations require an understanding of material behavior under mechanical stress. Detailers must account for material compression and stretch using K-factors and bend allowances, establishing strict tolerances for critical bends.
Holes, Cutouts, and Surface Preparation
Drawings must define precise hole sizes and locations for bolting, along with edge treatments, shearing/punching limits, and laser cutting paths.
Clutter Control
While drawings need to be comprehensive, adding excessive, non-fabrication details creates drawing clutter and confuses machine operators. Detailers must balance detail with readability.
DFM CHECKLIST FOR SHOP FLOOR
Standardizing Connection Details Across a Project
A large share of avoidable RFIs come not from any single wrong detail but from inconsistency — the same connection type detailed three different ways across a project because three different detailers each drew it from scratch. Building a shared connection-detail library at the start of a job, and requiring every detailer on the team to pull from it rather than redraw common connections, removes an entire category of shop-floor questions about why two supposedly identical connections don't match.
Measuring DFM Impact Over Time
The value of a DFM checklist is easiest to prove with a simple metric most shops already have the data for: RFIs per hundred drawings, tracked project over project. A shop that starts logging which DFM checklist item was missed on each RFI — missing weld access, an unreachable bolt, a tolerance not called out — builds its own prioritized list of which checklist items actually prevent the most rework, rather than treating every item on a generic checklist as equally important.
Getting Shop-Floor Feedback Into the Detailing Process
The most reliable source of new DFM checklist items isn't the drawing office — it's the shop floor. Welders, fitters, and machine operators encounter the gap between a technically correct drawing and a practically fabricable one every day, and a lightweight feedback loop (even something as simple as a shared list where shop staff can flag a recurring annoyance) surfaces DFM improvements that no amount of desk review would catch, because the detailer designing the checklist has usually never personally had to weld into the space they specified.
Closing that loop — reviewing shop feedback on a regular cadence and updating the DFM checklist accordingly — is what turns DFM from a one-time document into a checklist that keeps getting more useful project over project.
Balancing DFM Discipline with Design Intent
DFM guidelines exist to make fabrication easier, but they shouldn't be applied so rigidly that they override a genuine architectural or structural requirement the design actually needs. A detailer following a DFM checklist has to be able to recognize when a design intent — an exposed connection meant to be seen, a tight tolerance required for an adjacent finish — justifies deviating from the standard DFM guidance, and to flag that deviation clearly rather than either silently overriding the design or silently applying a DFM shortcut that compromises what the design was actually trying to achieve.
Frequently asked questions