Erection Drawings vs. Marking Plans: Accelerating Site Assembly by 30%
- Erection drawings show the high-level assembly: framework layout, member positions, section cuts and field bolt/weld callouts.
- Marking plans map every piece's unique mark onto a grid, with North orientation, elevations, purlin layouts and anchor locations.
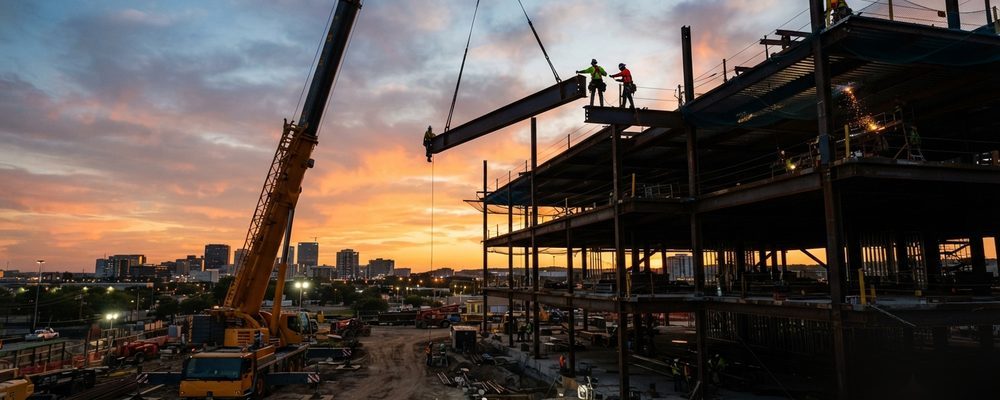
- Using both together eliminates field guessing and speeds up crane utilization during erection.
Field erection efficiency depends on drawing clarity. Field crews must quickly identify where each structural member belongs, its orientation, and how assemblies fit together.
Erection Drawings
High-level assembly plans showing structural framework layouts, member positions, section cuts, field bolt schedules, field welding callouts, and safety bracing details.
Marking Plans
Specialized layout plans that map every member's unique piece mark onto a master grid pattern. Marking plans include:Clear North orientation arrows for correct field alignment. Grid pattern overlays and centerline elevations. Purlin layouts and wall girt elevations. Anchor bolt and post-installed Chemset / Trubolt locations.
Site Productivity Impact
Combining Erection Drawings with clear Marking Plans eliminates field guessing, prevents member orientation errors, and speeds up crane utilization.
ERECTION MARKING PLAN ELEMENTS
Sequencing Erection Drawings by Zone or Pour
On any project large enough to erect in phases, erection drawings should be organized to match the actual erection sequence — by pour area, by bay, or by zone — rather than simply by piece mark order. A crew working zone 3 shouldn't have to flip through drawings for zones 1, 2, and 4 to find their pieces; splitting the erection set to mirror the steel erector's actual sequence plan cuts the time a crew spends just locating the right sheet, which on a fast-moving job adds up over a project.
Keeping Piece Marks Consistent Between Shop and Erection Sets
The marking plan and the shop drawings have to agree on piece marks down to the character, because a crane crew matching a tag welded to a beam against the marking plan has no way to know the shop drawing used a slightly different numbering convention. Any renumbering that happens during detailing — splitting a member, combining two short pieces, changing an assembly mark after a design revision — needs to propagate to both sets before either is released, which is why most shops treat piece-mark changes as a single workflow step that touches both documents together rather than two separate updates.
Handling Late Design Changes Without Breaking the Marking Plan
A design change that arrives after piece marks have already been assigned and steel is in fabrication is one of the highest-risk moments in the whole detailing process, because it threatens to desynchronize the marking plan from what's physically been cut and marked in the shop. The safer practice, once fabrication has started, is to avoid renumbering existing pieces wherever possible and instead assign new marks to only the changed or added members, even if that means the marking plan's numbering isn't perfectly sequential anymore — a marking plan that's slightly less tidy but matches reality is far more useful in the field than a renumbered one that no longer matches what's already stamped on steel sitting in the yard.
Field Verification Against the Marking Plan
Before a crew relies on a marking plan for a full day of picks, a brief field verification — confirming that a sample of piece tags in the laydown yard actually match what the marking plan shows for that zone — catches transcription errors or shipping mix-ups before they cost crane time. This is a small habit that costs a few minutes at the start of a shift and prevents the much more expensive outcome of a crew discovering a mismatch only after a piece is already rigged and halfway to its final position.
Frequently asked questions